The manufacturing of commercial and industrial cold storage doors is a specialized engineering discipline combining thermodynamics, polymer chemistry, and precision metallurgy. Low-grade cold doors constructed by manually gluing pre-cut insulation slabs or using low-pressure open-pour foam inevitably fail in service. Within months of commissioning, these inferior barriers develop internal voids, warping, and severe ice accumulation within the door core.
Understanding how cold storage doors are built reveals eight precise manufacturing stages. These include structural skeleton fabrication, high-pressure PIR foam injection, polyamide thermal break assembly, heating cable embedding, EPDM gasket extrusion, CNC drop-track machining, life safety integration, and six-stage factory quality testing. In over two decades of engineering heavy-duty entrance systems and custom cold room doors, factory engineering teams have evaluated thousands of industrial installations. Every manufacturing process is refined to guarantee long-term thermal efficiency and mechanical reliability.
1. Structural Skeleton & Internal 6063-T5 Framing
The foundation of any high-performance cold storage door begins with the design and fabrication of its internal structural skeleton.
Extruded 6063-T5 Perimeter Channel Fabrication
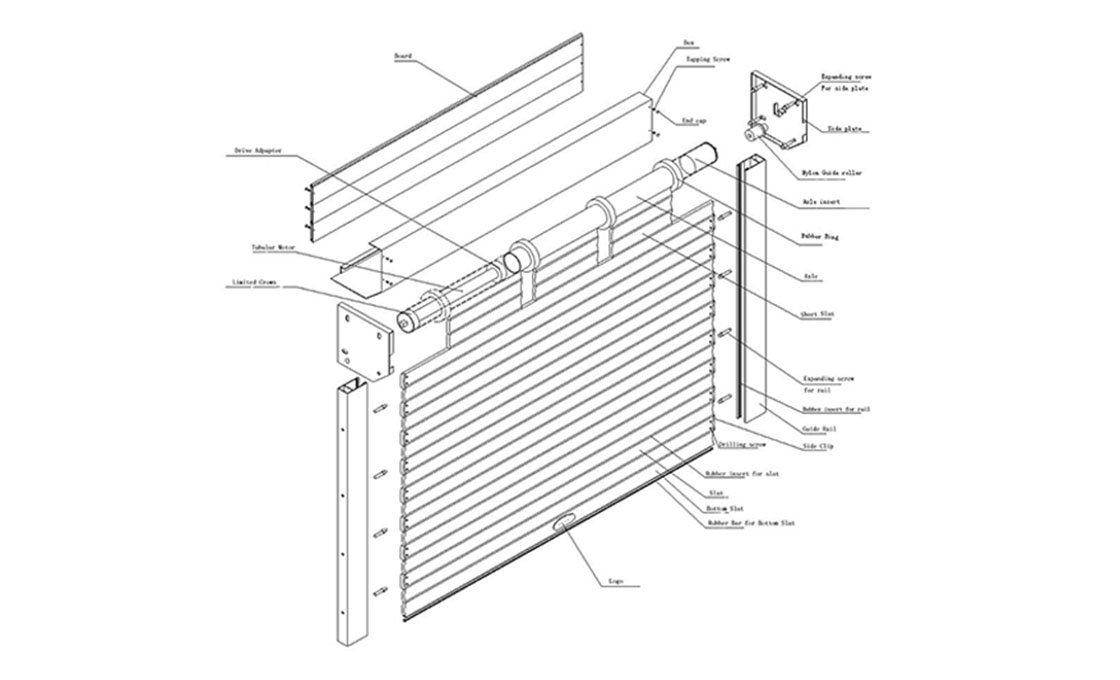
Modern cold room door leaves utilize heavy-duty 6063-T5 architectural aluminum perimeter sub-frames. Aluminum profiles are cut to sub-millimeter tolerances using automated dual-axis CNC miter saws. The corners are mechanically joined using heavy zinc-plated corner cleats and high-tensile fasteners. This creates a rigid structural boundary that resists torsional twisting during rapid forklift cycling.
Laser-Cut Reinforcement Plates for Load-Bearing Hardware
Prior to insulation foaming, technicians install 3.0 mm to 5.0 mm thick laser-cut 304 stainless steel reinforcement plates inside the perimeter frame at all critical stress points. These internal backing plates provide heavy anchoring for upper roller brackets, bottom guide shoes, internal locksets, and safety push rods. Anchoring hardware directly into internal steel reinforcement prevents fasteners from pulling out under extreme dynamic loads.
2. High-Pressure PIR Foam Core Injection & Curing
The core thermal barrier of a cold room door depends entirely on the chemical composition and injection mechanics of the polyisocyanurate (PIR) insulation foam. In studying how cold storage doors are built, foam injection technology represents the single most critical quality determinant.
High-Pressure Impingement Mixing at 150 to 200 Bar
Unlike cheap doors made with low-pressure pour foam, high-performance cold doors utilize high-pressure impingement injection heads. Polyol and isocyanate chemical streams are precisely metered and mixed under extreme pressure (150 to 200 bar). This high-velocity impingement atomizes the liquid mixture, ensuring uniform molecular cross-linking and a closed-cell content exceeding 95%.
Heated Hydraulic Press Curing at 50°C
The assembled metal door casing is clamped inside a 100-ton hydraulic heated platen press maintained at a constant 50°C. As the PIR foam expands within the cavity, the press restrains the outer metal skins. This continuous pressure ensures a uniform core density of 42 to 45 kg/m³ with zero internal voids or air pockets. Controlled curing delivers exceptional compressive strength and an ultra-low thermal conductivity of λ = 0.020 to 0.022 W/mK.
Looking for Custom Engineered Cold Storage Doors?
Send your facility opening dimensions, operating temperature delta, and cladding requirements to the factory engineering team for custom drawings and factory direct quotes.
3. Polyamide Thermal Break Framework Assembly
A critical stage in how cold storage doors are built is the fabrication of the perimeter thermal break framework.
Precision Crimping of PA66 GF25 Insulating Bars
Perimeter door frames are manufactured from two separate 6063-T5 aluminum extrusions: an outer casing facing the ambient warehouse and an inner rebate facing the refrigerated space. These two metallic sections are joined using 24 mm to 34 mm structural polyamide (PA66 GF25) insulating strips reinforced with 25% glass fiber. Automated rolling machines knurl the aluminum channels and crimp the polyamide bars with high mechanical pressure.
Finite Element Dew Point Barrier Verification
Polyamide exhibits a thermal conductivity of only λ = 0.30 W/mK, representing a 160-fold reduction in heat transmission compared to solid steel. This structural barrier isolates the exterior frame from sub-zero internal temperatures. It keeps exterior surfaces above the ambient dew point, eliminating frame condensation under 85% relative humidity.
4. Embedding Self-Regulating Anti-Frost Heating Cables
For sub-zero freezers and blast rooms, active perimeter heating is engineered directly into the door framework during factory assembly.
Dedicated Extruded Aluminum Heating Channels
Technicians route self-regulating semiconductor heating cables producing 25 to 35 Watts per linear meter. These cables run through dedicated snap-in aluminum channels along all four frame jambs and beneath the stainless steel floor threshold. Aluminum channels act as continuous heat diffusers, transferring thermal energy evenly across the perimeter gasket rebate.
Dual-Circuit Redundancy Wiring
In high-specification installations, dual independent heating circuits are installed side-by-side with an automated changeover relay. If the primary circuit experiences an electrical fault, the secondary backup circuit activates instantly. This redundancy prevents frame icing without requiring door disassembly.
5. Multi-Chamber Low-Temperature EPDM Gasket Installation
The perimeter sealing system is the primary mechanical barrier preventing warm air infiltration and convection energy loss.
Virgin Multi-Chamber EPDM Elastomer Co-Extrusion
Cold storage gaskets are co-extruded from virgin multi-chamber EPDM rubber formulated with paraffinic low-temperature plasticizers. This specialized elastomer maintains a glass transition temperature below -55°C. It ensures 100% mechanical elasticity and compression recovery across extreme operating ranges from -45°C to +80°C.
Snap-In Aluminum Retainer Channels
Gaskets are installed into extruded aluminum retaining channels rather than being glued. This snap-in design allows plant maintenance technicians to replace damaged gasket sections in minutes without removing the door leaf from its track.
6. Dual-Axis 45-Degree Drop-Track Kinematics Machining
The mechanical track system defines the kinematic movement of heavy sliding cold storage doors.
CNC-Milled 45-Degree Drop Notches
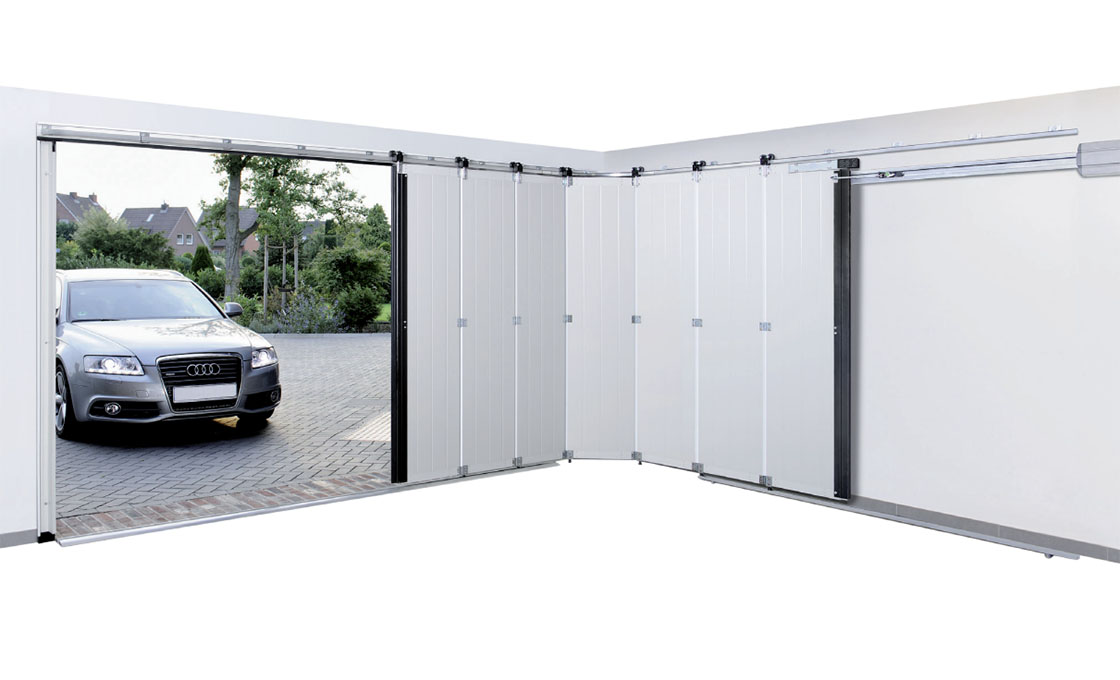
Heavy extruded aluminum overhead tracks are CNC-machined with precision 45-degree angled drop notches. During horizontal opening and closing travel, the door panel remains suspended 10 mm off the floor and 8 mm away from the frame, ensuring zero gasket friction and whisper-quiet operation.
Gravity-Assisted Compression Sealing
During the final 50 mm of closing stroke, high-load roller carriages glide down the 45-degree angled track ramps. Gravity lowers the door leaf 10 mm vertically and shifts it 8 mm horizontally inward against the frame, compressing multi-chamber EPDM gaskets hermetically against the stainless steel jambs.
7. Emergency Escape Hardware & Pressure Relief Valves
Life safety and atmospheric pressure equalization systems are integrated during final mechanical assembly.
Photoluminescent EN 179 Emergency Release Rods
All walk-in cold room doors incorporate an internal mechanical escape mechanism complying with EN 179 and OSHA safety codes. A solid stainless steel push rod extends through the insulated core to an interior glow-in-the-dark knob, allowing trapped personnel to escape immediately even if the exterior handle is padlocked.
Heated Bi-Directional Pressure Relief Ports
When warm air is ingested during transit and cools rapidly, volume contraction creates a vacuum of 200 to 500 Pascals. Bi-directional heated pressure relief valves equalize air pressure at ±25 Pa differentials, preventing door vacuum-lock and protecting insulated wall panels from structural deflection.
8. Six-Stage Factory Quality Assurance & Thermal Testing
Every cold storage door undergoes rigorous factory quality assurance testing prior to crating and global dispatch.
Infrared Thermal Imaging and Void Detection
Each cured door leaf is placed in a test chamber with a 30°C temperature delta. Calibrated infrared thermal imaging cameras scan the entire surface area to verify uniform thermal resistance and confirm zero internal foam voids or thermal leaks along the perimeter frame.
High-Voltage Insulation and Cycle Testing
Perimeter heating cables undergo 1,500V high-voltage dielectric withstand testing to verify electrical insulation integrity. Mechanical door assemblies are cycle-tested on automated test rigs for 10,000 continuous cycles to confirm smooth track kinematics and latch alignment.
9. Master Manufacturing Process Matrix: Cold Storage Doors
The manufacturing process matrix below summarizes the eight primary engineering stages involved in how cold storage doors are built:
| Manufacturing Stage | Engineering Process & Machinery | Quality & Compliance Standard |
|---|---|---|
| 1. Structural Skeleton | CNC miter cutting of 6063-T5 aluminum channels | Sub-millimeter dimensional tolerances |
| 2. High-Pressure Foaming | 150-200 bar PIR injection into 50°C press | 42-45 kg/m³ density; >95% closed cells |
| 3. Thermal Break Assembly | Automated rolling & crimping of PA66 GF25 bars | 24-34 mm non-conductive barrier (λ=0.30) |
| 4. Perimeter Heating | Embedding 25-35 W/m self-regulating cables | 1,500V dielectric insulation resistance test |
| 5. Gasket Co-Extrusion | Precision fitting of multi-chamber EPDM seals | -55°C glass transition temperature rating |
| 6. Track CNC Machining | CNC milling of 45-degree drop ramps on tracks | 10 mm drop / 8 mm inward dual-axis motion |
| 7. Safety Hardware | Fitting EN 179 escape rods & ±25 Pa relief ports | 100% mechanical override under external lock |
| 8. Factory Testing | Infrared thermography & 10,000 cycle rig run | Zero thermal bridging; CE & ISO compliance |
Manufacturing protocols and quality management guidelines established by ISO and workplace safety codes from the Health and Safety Executive ensure consistent thermal and mechanical performance across industrial cold storage installations.
10. Engineering Consultation for Custom Cold Room Door Fabrication
Understanding how cold storage doors are built empowers facility managers to select entrance systems engineered for extreme thermal performance and operational durability. Reviewing core insulation density, thermal break crimping, and track kinematics prior to procurement ensures reliable facility operations.
Need custom engineering drawings for cold storage doors?
If you are designing a specialized cold room or require customized door dimensions, the factory engineering team is available to review your operating parameters, clear opening specifications, and cladding requirements to provide comprehensive engineering submittals.
Frequently Asked Questions About Cold Storage Door Manufacturing
What insulation material is used inside cold storage doors?
High-performance cold storage doors utilize high-pressure injected, closed-cell polyisocyanurate (PIR) foam with a uniform density of 42 to 45 kg/m³.
Why is high-pressure foam injection critical during manufacturing?
High-pressure injection atomizes chemical streams at 150-200 bar, ensuring uniform density, zero internal voids, and a closed-cell content exceeding 95%.
How are thermal breaks installed in cold storage door frames?
Frames are constructed with inner and outer aluminum sections joined by 24 mm to 34 mm PA66 GF25 polyamide insulating bars crimped under high mechanical pressure.
Why are drop tracks machined with a 45-degree angle?
The 45-degree CNC drop ramps guide rollers to lower the door 10 mm vertically and 8 mm inward during closure, compressing seals without floor drag.
What factory tests are performed on cold storage doors before shipping?
Doors undergo infrared thermal imaging for void detection, 1,500V heating cable insulation tests, and mechanical cycle testing on automated test rigs.