Operating a temperature-controlled logistics facility without a disciplined preventive maintenance program leads to premature hardware failure. Facility managers frequently battle frozen door seals and torn rubber gaskets. In neglected facilities, bent roller carriages and overloaded refrigeration compressors cut a 15-year door lifespan down to less than four years.
Mastering how to extend the lifespan of your cold room doors requires systematic maintenance across seven engineering checkpoints. Key areas include gasket health, heating continuity, -50°C lubrication, track calibration, bollards, pressure relief ports, and structured inspection cadences. In over two decades of engineering heavy-duty entrance systems and industrial cold room doors, field engineering teams have evaluated thousands of facilities. Plant managers who execute structured preventive maintenance reduce emergency service call-outs by 85% and extend operating equipment life beyond 15 to 20 years.
1. Routine Inspection and Replacement of EPDM Gaskets
The perimeter rubber gasket represents the first line of defense against warm ambient air infiltration and humidity migration.
Daily Visual Checks and the Dollar-Bill Compression Test
Inspect perimeter gaskets daily for localized cracking, physical tearing, or permanent compression set. Conduct the standard compression test by closing the door on a standard paper currency bill at multiple points around the frame. If the paper pulls out easily without firm friction, the gasket has lost its compression recovery and must be adjusted or replaced immediately.
Snap-in Gasket Replacement and Corner Vulcanization
High-quality cold room doors utilize snap-in aluminum retaining channels. When replacing worn gaskets, technicians can pull the damaged profile free and press a new virgin multi-chamber EPDM seal into the channel without unmounting the heavy door panel. Ensure factory-molded 90-degree corner joints are used rather than crude mitre cuts to prevent corner air leaks.
Additionally, technicians should wipe gasket contact surfaces weekly with a mild food-safe sanitizing solution to remove ice crystals and spilled organic liquids. Accumulations of dirt or grease accelerate polymer degradation, causing rubber profiles to harden and crack prematurely.
2. Electrical Heating Circuit Diagnostics & Resistance Testing
In sub-zero freezer enclosures (-18°C to -35°C), failure of the perimeter heating cable leads to rapid ice formation. This frost glues rubber gaskets to the metal frame, causing instant seal tearing upon door opening.
Monthly Line Resistance and Current Draw Measurements
Measure the electrical resistance (Ohms) and current draw (Amps) of all perimeter frame and floor threshold heating circuits on a monthly schedule. Compare measured values against the manufacturer nominal rating (typically 25 to 35 W per linear meter). A significant spike in resistance indicates heating core micro-fractures, while zero current indicates a tripped breaker or severed cable.
Infrared Thermal Imaging Inspections
Utilize a handheld FLIR thermal imaging camera during quarterly audits. An active, healthy heating cable displays a uniform warm outline (+5°C to +8°C) along the entire door jamb and threshold plate. Cold dark spots on the thermal scan reveal localized heating failures before visible ice build-up damages the door hardware.
If heating cable replacement is required, always verify that the replacement wire matches the exact electrical specifications of the original installation. Installing heating elements with excessive wattage can cause thermal degradation of surrounding polyurethane insulation, while undersized wires fail to prevent ice build-up during peak humidity cycles.
Need Replacement Parts or Engineering Door Audits?
Send your facility door specifications, temperature delta, and daily cycle counts to the technical support team for factory-direct replacement gaskets, heating cables, or custom retrofit panels.
3. Low-Temperature Lubrication for Mechanical Hardware (-50°C)
Standard industrial lubricants solidify into hard, abrasive waxy pastes when exposed to sub-zero temperatures, causing bearing lockups and roller track gouging.
NSF-H1 Synthetic Low-Temperature Greases
Always apply specialized synthetic low-temperature grease formulated for extreme cold environments (-50°C to +120°C). Ensure the lubricant carries NSF-H1 food-grade certification for facilities processing meat, dairy, or pharmaceutical goods. Lubricate sliding roller bearings, cam-lift hinge spiral tracks, guide shoes, and latch pivot points every quarter.
Cleaning Tracks Prior to Lubrication
Never apply fresh grease over contaminated, debris-laden roller tracks. Wipe extruded aluminum guide tracks with clean industrial degreasing cloths to remove accumulated dust, ice flakes, and worn metallic particles before applying a thin, uniform film of synthetic lubricant.
Maintenance technicians should also inspect manual cam-lift spiral hinges and motorized drive chain tensioners every six months. Adjusting mechanical backlash prevents eccentric loads from wearing out internal brass bushings and roller bearings.
4. Track Alignment & Drop-and-Inward Kinematics Calibration
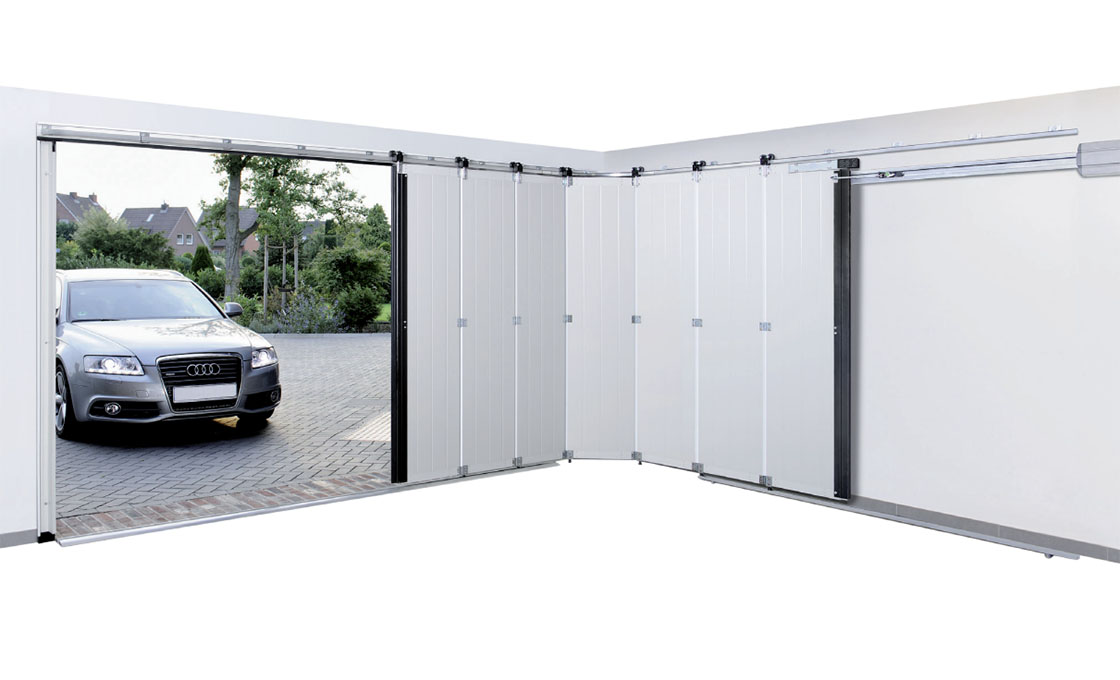
Heavy sliding cold storage doors rely on dual-axis drop-and-inward kinematics to compress perimeter seals hermetically without dragging across the frame during travel.
Calibrating the 10mm Drop and 8mm Inward Stroke
Over thousands of operational cycles, foundation settling or mounting bolt vibration can cause guide tracks to drift out of level. Verify that the door drops exactly 10 mm vertically and moves 8 mm inward in the final 150 mm of closing travel. Adjust the eccentric roller axle bolts to ensure the door leaf presses evenly against both vertical jambs simultaneously.
Bottom Guide Shoe Clearance Inspection
Inspect the concealed floor guide shoes located at the lower corners of the door leaf. Ensure the guide shoe maintains 2 mm to 3 mm of operational clearance inside the bottom aluminum channel. Excessive play allows the door leaf to sway during forklift passage, damaging top trolley bearings.
When training maintenance staff on how to extend the lifespan of your cold room doors, emphasize verifying track stop blocks and hydraulic buffers. Properly calibrated end-stops absorb horizontal momentum smoothly, preventing structural shock loads from fracturing overhead mounting anchors.
5. Physical Bollard Impact Protection & Traffic Management
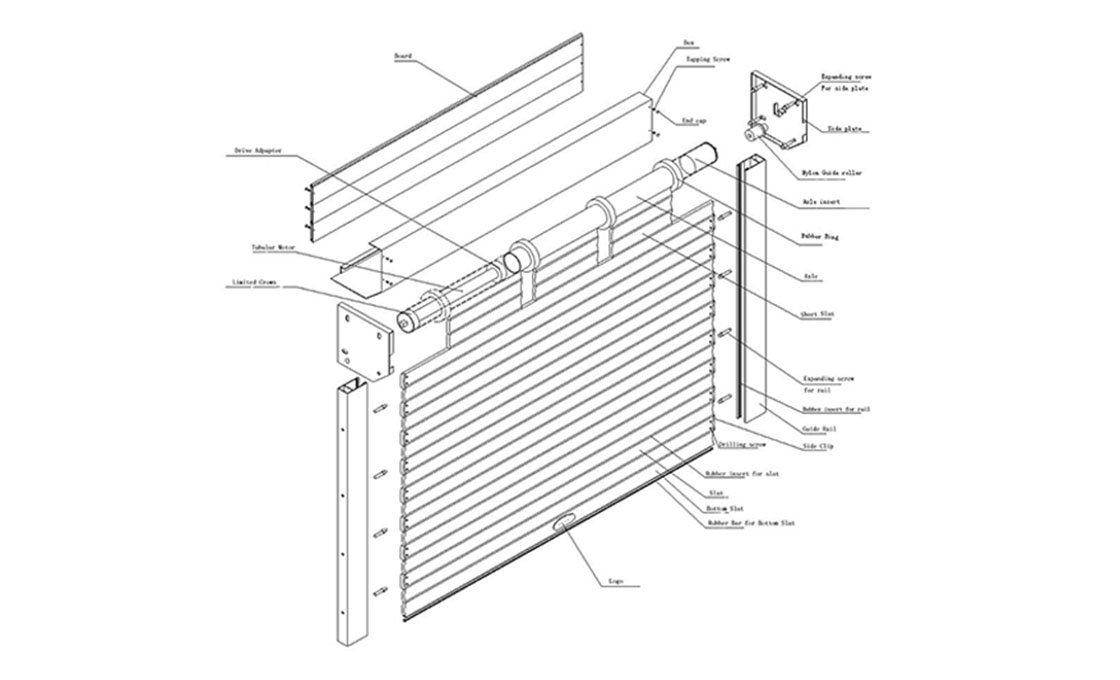
Accidental impacts from forklifts and motorized pallet jacks account for over 60% of catastrophic structural failures in commercial cold storage facilities.
Installing Heavy-Duty Structural Steel Bollards
Protect door frame jambs by anchoring 150 mm diameter concrete-filled structural steel bollards 150 mm forward of the opening on both the warm and cold sides. Bollards should feature high-visibility yellow powder coating and stand at least 1000 mm high to deflect forklift wheel hubs and pallet corners safely.
Automated Radar and Motion Sensor Activation Zones
Configure automated door radar detectors and floor induction loops to activate with sufficient approach distance (3 to 5 meters). This allows the door to reach full open height before the forklift reaches the threshold, eliminating glancing impacts against the lower door edge.
Additionally, install high-visibility warning lights and audible alarms synchronized with automated door movements. Visual indicators alert forklift operators when the door is in motion, reducing the risk of premature bay entry and protecting sensitive safety photocell sensors from pallet damage.
6. Pressure Equalization Valve Inspection & Defrosting
When a large walk-in freezer door closes, the rapid cooling of newly ingested warm air creates an intense internal vacuum that can deflect door panels or pull ceiling panels down.
Testing Bi-Directional Flapper Movement
Two-way pressure equalization valves utilize spring-loaded flappers calibrated to open at ±25 Pa pressure differentials. Inspect the internal valve flappers quarterly to ensure they swing freely in both positive and negative pressure directions without mechanical binding.
Verifying Internal Valve Heating Elements
Pressure valves incorporate built-in 15W to 25W heating elements to prevent moisture from freezing the flapper shut. Verify electrical continuity on the valve heater during cold season preparations to prevent destructive pressure imbalances.
In addition, clean the external protective mesh screens on pressure relief ports every six months. In food processing environments, airborne dust and ice crystals can clog vent passages. This debris restricts airflow, forcing refrigeration door gaskets to absorb destructive hydraulic shock waves.
7. Preventive Maintenance Checklist: Daily, Monthly & Annual SOPs
Implementing a structured schedule is the most effective strategy when determining how to extend the lifespan of your cold room doors:
| Maintenance Frequency | Inspection Tasks & Action Items | Pass / Fail Standard |
|---|---|---|
| Daily Inspection | Visual check of EPDM gaskets, door smooth travel, floor threshold clear of ice | Zero seal tearing; zero ice accumulation; smooth manual/electric motion |
| Monthly Inspection | Measure heating cable resistance; test emergency inside safety release push rod | Heater draws 25-35 W/m; emergency knob releases locked door effortlessly |
| Quarterly Inspection | Apply -50°C NSF-H1 grease to hinges/rollers; test pressure relief port flappers | Clean tracks; free flapper movement at ±25 Pa; zero bearing grind |
| Annual Inspection | Re-calibrate drop-and-inward track kinematics; tighten anchor bolts; thermal scan | Uniform 10mm drop / 8mm inward seal; zero cold bridge leaks on FLIR |
Workplace safety regulations from the Health and Safety Executive and quality standards from ISO mandate documenting all service logs for commercial refrigerated facilities. Maintaining audited maintenance records ensures compliance with cold chain certification standards and validates equipment warranty coverage.
8. Engineering Overhaul Consultation for Your Facility
Understanding how to extend the lifespan of your cold room doors requires regular inspections, prompt component replacements, and scheduled calibration. Adhering to these preventive engineering protocols guarantees continuous temperature protection and lowest total lifecycle operating costs.
By enforcing daily visual checks, monthly heating circuit tests, and quarterly low-temperature synthetic lubrication, facility managers protect multimillion-dollar cold chain assets and eliminate unexpected refrigeration equipment overhauls.
Need technical assistance establishing a cold room door maintenance program?
If your facility is experiencing recurring gasket freezing, track misalignment, or excessive refrigeration energy losses, the technical support engineers are available to review your facility door schematics and provide customized maintenance SOPs and OEM replacement parts.
Frequently Asked Questions About Cold Room Door Maintenance
What type of lubricant should be used on cold room door hinges?
Always use synthetic low-temperature NSF-H1 food-grade grease rated down to -50°C. Standard petroleum grease solidifies in freezing temperatures and locks bearings.
How often should cold storage door gaskets be replaced?
High-quality EPDM gaskets typically last 3 to 5 years under normal operation. Replace gaskets immediately if they show tears, permanent compression set, or fail the paper test.
Why is my freezer door freezing shut?
Freezer doors freeze shut when the perimeter heating cable fails, heating circuit voltage drops, or damaged gaskets allow warm humid air to penetrate and freeze on the cold frame.
How do you test a cold room door emergency safety release?
Padlock the exterior door latch, enter the cold room, and firmly push the interior glow-in-the-dark safety knob. The latch must disengage immediately without electrical power.
What causes sliding cold room door tracks to wear out quickly?
Tracks wear out prematurely due to lack of -50°C synthetic lubrication, debris accumulation, misaligned drop-and-inward kinematics, or repeated forklift collisions.